Hey there, I’m Jake, been working with shrink packaging machines for over a decade now—first on the factory floor troubleshooting breakdowns, now running the supplier side where I talk to packaging teams every single day. One question I get nonstop from folks testing or upgrading their line is: “What actually matters for the packaging when we run it through a shrink wrapper?” It’s not just about slapping plastic around a box and calling it good, y’know? Get the appearance right, and your finished goods look sharp, pass QC, and even save you money on wasted film. Mess it up, and you’re dealing with wrinkled junk, seams splitting, or products getting stuck together. Let’s break down what I see day in and day out that makes or breaks the final shrink packaging look. Shrink Packaging Machines
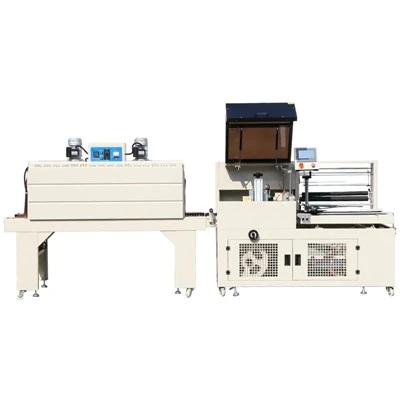
First up, the star of the show: film specs. A lot of new customers think “shrink film is shrink film, right?” Nope. Big mistake. Most of us supply both the machines and matching films, and I can’t tell you how many times a guy buys a generic roll of plastic from the local industrial supply shop, throws it on our machine, and texts me panicking because everything looks like a crumpled soda can. Let’s get specific. For most standard applications—singles of snacks, small electronics, retail boxes—you’re looking at PVC or POF (polyolefin) film. PVC’s cheap, shrinks tight, works great for rigid items, but it’s got that off-gas smell sometimes and can yellow if it sits on a shelf too long. POF’s the go-to now for most food, cosmetics, and high-end retail because it’s clear, shrinks evenly, no weird odors, and works for curved items too. But here’s the key number people sleep on: shrink ratio. That’s how much the film pulls in when heated. For most boxes, you want 25-35% linear shrink ratio. Too low, and you’ll have loose, baggy film that wrinkles like a old blanket. Too high, and the film stretches too thin, seams split, or it pulls so tight it warps the product—like a DVD case bending in a too-tight shrink wrap.
Then there’s film gauge, which is just thickness. For light stuff like candy bars or makeup samples, you’re good with 40-50 gauge. Heavy items like cases of soda or industrial parts need 60-75 gauge so the film doesn’t tear when it’s handled after packaging. I had a customer last month who ran 50-gauge film on a case of canned beans, and every other case had a split seam. Switched to 65-gauge, and he hasn’t had a single issue since. Pro tip from my team: always match the film’s “shrink temperature range” to your machine’s heat settings. If your machine’s heat tunnel runs at 250°F, don’t buy film that needs 300°F to shrink—you’ll either have half-shrink mess or burn holes in the plastic.
Next, the product itself. You can have a perfect film and a top-tier machine, but if your product isn’t prepared right, the final look is garbage. Let’s start with dimensions. First, length and width of the bundle. If you’re wrapping a single box, don’t just grab film and wrap it—measure how much overlap you need for the seam. Almost all shrink machines (especially the semi-automatic ones most small to mid-sized shops use) need 1.5-2 inches of film overlap on the side seam. If you don’t leave that extra, the sealer can’t melt the two layers together, and the seam splits the second it hits the heat tunnel. I see this all the time: a guy cuts the film exactly to the product size, runs it, and calls me saying “your machine is broken, seams won’t stick.” Nah, buddy, you forgot the overlap.
Then there’s the shape and surface texture of the product. Smooth, rigid boxes? Easy—film pulls tight, wrinkles only happen if the heat is off. But if you’re wrapping something with curved edges, like a water bottle, or textured, like a corrugated box with ridged edges? You’ve got to make sure the film conforms without trapping air or wrinkling. Air pockets are a huge pet peeve for packaging teams—they look unprofessional, and if they’re big enough, they make the film bulge. How to fix that? A lot of semi-automatic machines have a “tunnel pre-heat” or a vacuum feature, but even better, make sure the product isn’t damp or dusty before packaging. Moisture on the product makes steam get trapped under the film, leading to bubbles. Dust? It gets between the film and product, creating little white specks you can’t buff out. I once had a food client who tried wrapping warm cookies straight from the oven—steam under the film made everything look like it had mold spots. They waited 10 minutes for the cookies to cool, and the shrink look went from trash to award-worthy.
Heat settings are the next big one, and this is where a lot of new operators guess wrong, which kills the appearance. Let’s break down the two main heat zones on shrink machines: the sealer bar and the heat tunnel. The sealer bar has to melt the film layers together evenly, without burning them. If the sealer is too hot, the film gets charred, leaving brown marks on the package that look terrible. Too cold, and the seam is weak, like I mentioned earlier. For most POF film, sealer temp is around 275-300°F. Test it first: run a small sample, pull the seam, if it comes apart easily, crank it 10 degrees. If it leaves a brown smudge, turn it down.
Then the heat tunnel is where the magic happens—this is when the film shrinks tight around the product. If the tunnel temperature is too low, the film won’t shrink all the way, leaving loose, baggy areas that wrinkle. Too high, and the film shrinks too fast—crinkles, bubbles, or even melts into the product (ask me how I know about a melted lipstick tube once). What’s the sweet spot? Again, for POF, it’s usually 300-325°F. And don’t forget tunnel speed! If your conveyor moves too fast, the film doesn’t have enough time to shrink evenly. Too slow, and you overheat the product and the film. I tell every customer to adjust speed and temp together, not just one or the other. Do test runs with a few scraps of film and a sample product before running a full batch—saves you hours of rework.
Seal quality is something I see overlooked all the time, and it’s a huge part of appearance. Most shrink machines use either a straight seal bar or a impulse seal (the ones that heat quickly and pulse). First, the seal has to be straight—no crooked edges sticking out, because that looks messy. If your seal is crooked, it’s usually because you loaded the film roll off-center on the machine. The film should feed evenly on both sides, so check that guide rollers every time you change a roll. Also, make sure the seal bar is clean. Dried film residue builds up on the bar over time, which leaves little bumps or tears on the seal. Wipe the seal bar with rubbing alcohol once a week, easy—takes 2 minutes, saves you a ton of bad packages.
Wait, what about printed products? A lot of customers wrap boxes with logos or text, and they want that print to look sharp after shrink, not distorted. Big thing here: shrink film clarity. If you’re using cheap, hazy film, the print will look faded, even if it’s perfect before wrapping. Go for a high-clarity POF film if print is important to you. Also, make sure the shrink direction matches the product orientation. Film shrinks along its “machine direction” (the direction it feeds off the roll) more than cross direction. So if you have a long product, like a 12-inch pen box, you want the machine direction of the film to run along the length of the box, so it shrinks evenly side to side, not stretching the printed end. If you get that backwards, you’ll have text stretched or logos squished.
I also can’t skip talking about tension control. That’s the setting on the machine that pulls the film tight as it’s being wrapped around the product. Too much tension, and the film stretches too thin, leading to tears or warped products. Too little tension, and the film is loose, leading to wrinkles. Most modern machines have auto-tension, but if you’re using a semi-automatic, you’ve got to adjust it for each film type. I had a customer last month who kept getting wrinkled shrink packs and thought the machine was bad—turns out he was using old, manual tension that was way too low. Cranked it a little, and the wrinkles were gone. Game. Changer.
What about common appearance issues I see every week? Let’s tackle them, because that’s what most people actually care about. First, wrinkles. Usually that’s from either bad tension, wrong film shrink ratio, or uneven heat. If it’s on the sides, check tension. If it’s on the top or bottom of the bundle, heat tunnel temp is probably off, or the product isn’t sitting flat on the conveyor. Bubbles? Most often moisture or trapped air. If it’s small, you can poke a tiny pinhole in the film after shrink to let the air out, but bigger ones mean you need to dry the product or adjust the vacuum on the machine. Seam splits? Either not enough overlap, sealer too cold, or the seal bar is dirty. Burn marks? Sealer too hot, or film sitting on the bar too long when the machine’s idling.
And here’s a pro tip I only tell my regular customers: don’t skip the cooling step. A lot of operators pull the product straight out of the heat tunnel and stack it, and that’s when you get wrinkles or sagging. Shrink film needs to cool for 5-10 seconds after the tunnel to set tight. Some machines have a cool air blower built in, but if yours doesn’t, just lay the packages on a flat, hard surface (like a metal table, not a soft cardboard box) to cool. Do that, and the final look stays crisp, not messy.
Wait, let’s not forget about regulatory stuff if you’re in food or pharmaceuticals. Some shrink films have to meet FDA standards for direct food contact, right? If you’re wrapping granola bars or vitamins, the film can’t have any weird chemicals that leach into the product, and the packaging appearance might have to meet certain labeling requirements too. I always tell food clients to confirm their film is approved for their use, because a bad film not only looks bad, it can get your products pulled from shelves.
At the end of the day, the whole point of getting the packaging appearance right is to make your product look valuable. A nice, tight, clear shrink pack makes a $5 lipstick look like $15, while a wrinkled, bubbled pack makes even a $20 power tool look cheap. I see customers save 10-15% on rework costs just by getting the packaging and machine settings right, which is huge for small to mid-sized runs.
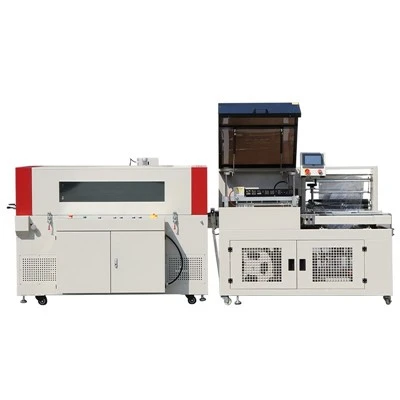
If you’re testing a new shrink machine or having issues with your current runs, don’t guess your way through it. My team and I work with all kinds of industries, from craft bakeries to automotive parts suppliers, so we’ve seen every possible appearance issue. We’ll walk you through film specs, machine settings, product prep—whatever you need to get that perfect, clean shrink look for your products. Hit us up whenever you’re ready to troubleshoot or talk through your specific packaging needs.
Smart Packaging Systems References:
- Shrink Film Technology: Properties and Applications, Packaging World, 2022
- "Shrink Packaging Appearance Standards for Retail Goods", National Association of Packaging, Processing, and Distribution Technology, 2023
- Operational Guidelines for Semi-Automatic Shrink Wrapping Machines, International Society of Packaging Professionals, 2021
Langfang Huanqi Machinery Equipment Co., Ltd.
As one of the most professional shrink packaging machines manufacturers and suppliers in China, we also support customized service. Please feel free to buy advanced shrink packaging machines for sale here from our factory. Quality products and reasonable price are available.
Address: No. 40, Row 11, North Side of Central Street, Wangpeizhuang Village, Pingshu Town, Dacheng County, Langfang City, Hebei Province
E-mail: huanqijixie@outlook.com
WebSite: https://www.huanqiwrap.com/
